Informations
PVA Water-Soluble Film Supports More Controlled Packaging Design
Packaging material selection is increasingly influenced by more than visual presentation or containment alone. Manufacturers must consider handling, dosing, compatibility with the packed product and the intended end-of-use process. PVA/PVOH water-soluble film has become a relevant option for specialized applications where a film is required to dissolve in water under defined conditions.
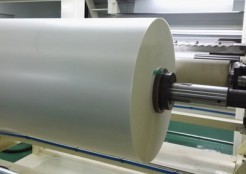
DUTE Protective Film develops PVA water-soluble film products for packaging and other application-focused uses. The material is formed from water-soluble polymer materials and can be specified according to the conditions of the intended use. For packaging operations, this creates an opportunity to combine containment with controlled handling in a single material format.
Supporting Unit-Dose and Specialist Packaging Applications
Water-soluble film is especially relevant to products where measured portions, reduced direct contact or simplified handling are important. DUTE identifies applications including agrochemicals, dyes, cements, food additives, seeds, laundry-related products and powder or liquid detergents. The exact requirements vary by product, but the principle remains the same: the packaging material should support the process rather than introduce unnecessary handling steps.
For unit-dose applications, the film can help create consistent packs while supporting more organized dispensing. In specialist industrial settings, it can also be considered where operators need to handle materials in predefined quantities. Product compatibility, storage conditions and water-dissolution requirements should always be evaluated for the specific application before final material selection.
Technical Considerations Matter
A successful PVA packaging project depends on more than choosing a water-soluble film. Manufacturers should consider the required dissolution profile, packaging method, seal performance, product characteristics and anticipated storage environment. These variables influence whether a specific film grade is suitable for a given line or product.
DUTE states that its water-soluble film offers characteristics including tensile strength, flexibility and heat-sealing capability for packaging applications. Its broader experience across protective and water-soluble film categories gives customers a practical starting point for discussing product requirements, dimensions and application conditions.
Partnering for Application-Focused Film Selection
As packaging expectations evolve, suppliers and manufacturers benefit from early technical discussion. Defining the packed material, the desired pack format and the intended handling process at the outset can help reduce uncertainty during later development stages.
DUTE Protective Film provides PVA/PVOH water-soluble film alongside its PE surface-protection portfolio. To explore material suitability for packaging, unit-dose or specialist handling applications, visit DUTE’s PVA packaging film page.